
Satisfies 1 requirement
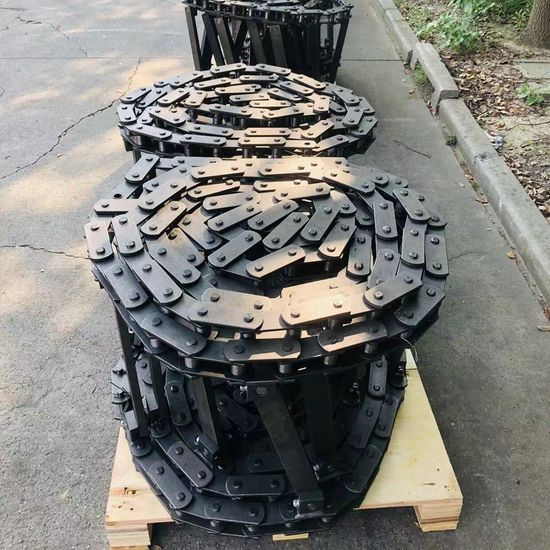
Bi-Planar Cardan Conveyor Chain for Caldan Conveyor System for Optimized Production Lines
US$50.00-80.00
100 Meters(MOQ)
I have found results from200000+products and80000+suppliers aboutConveyor system chain




When sourcing conveyor chains, you must prioritize tensile strength and fatigue resistance to ensure the system can handle the required load without elongation. Key specs include the pitch size, roller diameter, and plate thickness. For heavy-duty industrial use, ensure the chain is made from high-grade alloy steel or stainless steel (304/316) if corrosion resistance is required. Additionally, verify the breaking load (kN) meets your safety factor requirements, typically 7:1 or higher for overhead conveyors.
Compatibility hinges on the ISO, ANSI, or DIN standards the chain follows. You must confirm the attachment types (e.g., K-type, A-type, or extended pins) and their spacing intervals. It is highly recommended to request CAD drawings from the supplier to verify the sprocket engagement and ensure the width between inner plates matches your current drive system to prevent premature wear or derailment.
Suppliers should ideally hold ISO 9001:2015 certification for quality management. For specific industries, look for SGS or TUV inspection reports. If the chain is used in food processing, it must be FDA compliant and use food-grade lubricants. For mining or hazardous environments, check for ATEX certification to ensure spark-resistance and operational safety.
Longevity depends on the lubrication system (manual, drip, or oil bath) and the operating environment. For high-dust environments, specify self-lubricating chains with sintered bushings. Regular elongation monitoring is critical; a chain is generally considered worn out when it reaches 1.5% to 3% elongation. Ensure the supplier provides a maintenance manual detailing the recommended lubricant viscosity and tensioning intervals.
To avoid 'soft' steel or poor heat treatment, always require a Material Test Certificate (MTC) according to EN 10204 3.1. For large-scale projects, utilize third-party pre-shipment inspections (such as those offered via Made-in-China.com) to conduct hardness tests (HRC) and tensile strength verification before the balance payment is released.
Focus on the Total Cost of Ownership (TCO) rather than just the unit price. Negotiate for spare parts inclusion (e.g., connecting links and offset links) at no extra cost. If you have high annual volume, propose a blanket purchase order to lock in steel prices, as raw material fluctuations can impact costs by 10-20% annually. Request a warranty period of at least 12-18 months.
Conveyor chains are heavy and prone to surface rust during sea transit. Ensure the supplier uses anti-rust oil coating and wraps the product in VCI (Volatile Corrosion Inhibitor) film. Chains should be packed in reinforced seaworthy wooden crates (IPPC heat-treated) with a maximum weight per crate that matches your warehouse's forklift capacity to prevent handling accidents.
Always use secure payment methods and prioritize suppliers who are Audited Suppliers on Made-in-China.com. This ensures the company has been verified on-site by independent inspection companies. Avoid paying via untraceable methods; instead, use Letter of Credit (L/C) for very large orders or Escrow-based trade terms to ensure funds are only released upon proof of shipment.